
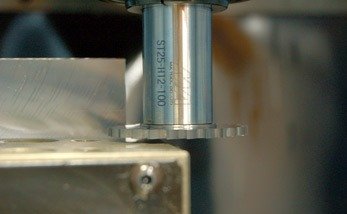
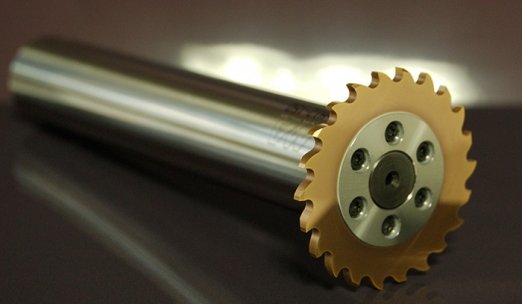
Make the carbide solid metal saw easier to use and perform higher performance with the machining machine. This concept led to the development of the SHARP SAW FZ. Until now, when installing metal saws on machining machines, using commercially available arbors would sometimes interfere with the vise, jig, or part of the workpiece that is packing, causing the arbor tightening nuts to interfere, which was cumbersome. The SHARP SAW FZ eliminates interference issues with its unique dedicated shank and clamp method, allowing it to clamp into a regular milling chuck for machining, just like an end mill. Additionally, the specifications of the metal saw can be adjusted according to the workpiece material, enabling highly efficient handling of various machining processes.
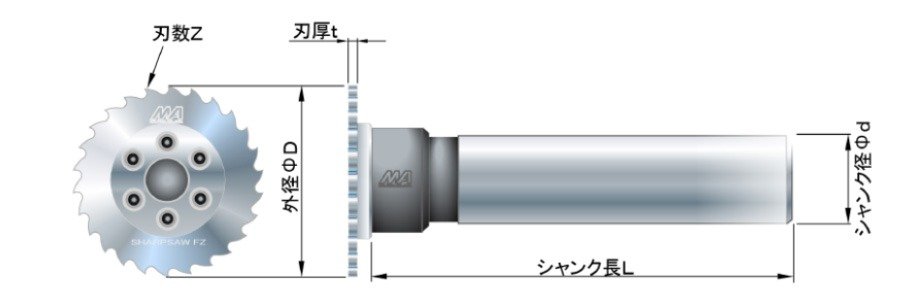
No protruding tip, allowing processing even at the very edge of the clamp jig!
assembly
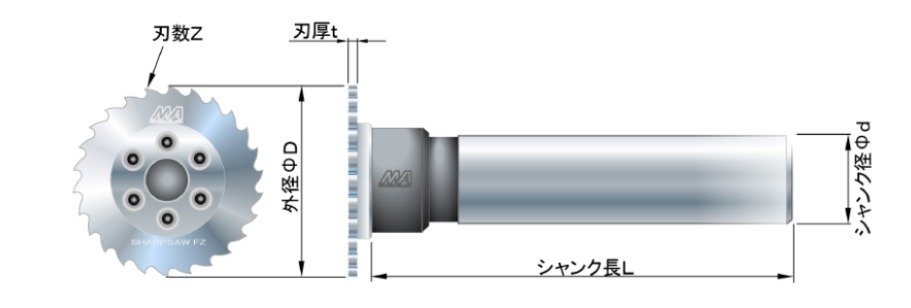
| Type | Outer diameter ΦD | Blade thickness t | Number of Blades Z | Shank diameter Φd | Shank length L | ||||
|---|---|---|---|---|---|---|---|---|---|
| P2.0 | P2.85 | P4.0 | P6.5 | P7.85 | |||||
| FZAL
FZHD
FZST
|
20 | User specification
0.3t~4.0t
(For outer diameter Φ20, ~3.0t)
Standard tolerance ± 0.005
|
30 | 22 | 16 | 12 | 100L | ||
| 25 | 40 | 28 | 20 | 16 | 100L
150L
|
||||
| 30 | 48 | 32 | 24 | ||||||
| 35 | 38 | 28 | 16 | 20 | |||||
| 40 | 44 | 32 | 20 | ||||||
| 45 | 36 | 22 | 18 | 25 | |||||
| 50 | 40 | 24 | 20 | ||||||
| 65 | 50 | 32 | 26 | 32 | |||||
solid metal saw
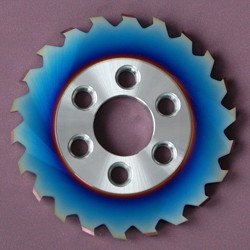
FZAL
For aluminum alloys, pure copper, and resin materials. Ideal for machining ductile materials such as
aluminum alloys.
It offers extremely high chip discharge and a sharp squeeze angle for high-quality processing with minimal
burrs.
The use of ALX coating prevents welding, allows high-speed processing, and maintains sharp sharpness
for long periods.
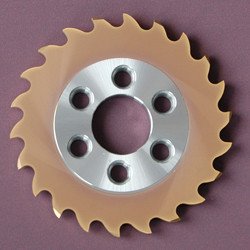
FZHD
For
stainless alloy, titanium alloy, and alloy steel. Ideal for difficult-to-machine materials such as stainless and titanium alloys.
Blade shape combining smooth chip discharge with cutting edge rigidity.
Uses a DMX coating with high hardness and high heat resistance, enabling
high-speed processing and long service life.
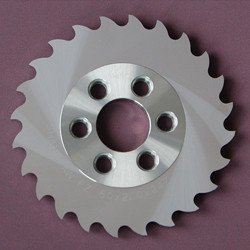
FZST
For general carbon steel~ Solid product without
coating.
The shape and specifications are mainly made of typical carbon steel.
We achieve smooth processing while keeping costs down.
| Type | Outer diameter ΦD | Blade thickness t | Number of Blades Z | ||||
|---|---|---|---|---|---|---|---|
| P2.0 | P2.85 | P4.0 | P6.5 | P7.85 | |||
| FZAL
FZHD
FZST
|
20 | User specification
0.3t~4.0t
(For outer diameter Φ20, ~3.0t)
Standard tolerance ± 0.005
|
30 | 22 | 16 | ||
| 25 | 40 | 28 | 20 | ||||
| 30 | 48 | 32 | 24 | ||||
| 35 | 38 | 28 | 16 | ||||
| 40 | 44 | 32 | 20 | ||||
| 45 | 36 | 22 | 18 | ||||
| 50 | 40 | 24 | 20 | ||||
| 65 | 50 | 32 | 26 | ||||
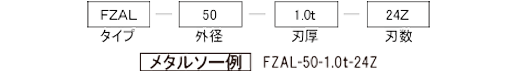
- For blade specifications and matching with machining, please contact us. We will propose the optimal specifications.
- We can also accommodate special shaped blades such as R-edges, V-shapes, and C-face blades.
- If you let us know your requirements such as machining depth, we will propose the number of blades.
shank section
| Product Number | Compatible metal saw outer diameter |
|---|---|
| ST12-H4-100L | Outer diameter Φ20 |
| ST16-H6-100L | Outer diameter: Φ25, Φ30 |
| ST16-H6-150L | |
| ST20-H8-100L | Outer diameter: Φ35, Φ40 |
| ST20-H8-150L | |
| ST25-H12-100L | Outer diameter: Φ45, Φ50 |
| ST25-H12-150L | |
| ST32-H15.875-150L | Outer diameter: Φ65 |
| ST32-H15.875-200L |
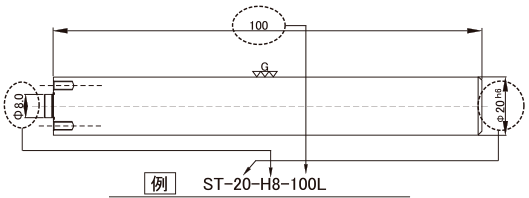
- BT shanks and HSK shanks can also be custom-made.
cutting conditions
| Processing Materials | V: Cycle speed (m/min) | fz: Cutting amount per tooth | Calculation method |
|---|---|---|---|
| Carbon steel (S45C) | 60~120 | 0.005~0.03 | V = (Outer diameter D×3.14× rotation speed N) / 1000
Feed speed Vf = fz×N×Z
N: Speed of rotation Z: Number of blades
|
| SUS304 | 40~100 | 0.005~0.002 | |
| titanium alloy | 40~100 | 0.01~0.03 | |
| SUJ2 | 30~90 | 0.005~0.02 | |
| Aluminum alloy | 200~500 | 0.005~0.02 |
- Please adjust the above cutting conditions according to workpiece rigidity and machine rigidity.
For setting the cutting amount per blade, if the first pass is deep, set it small; if the cut is shallow, set it large. - Please use it as a basic downcut for use.
- Due to the characteristics of the cutter, it is better to use cutting fluid for processing.
